
Case Study · Asphalt & Bitumen
Tank-Heating Burner for an Asphalt Farm
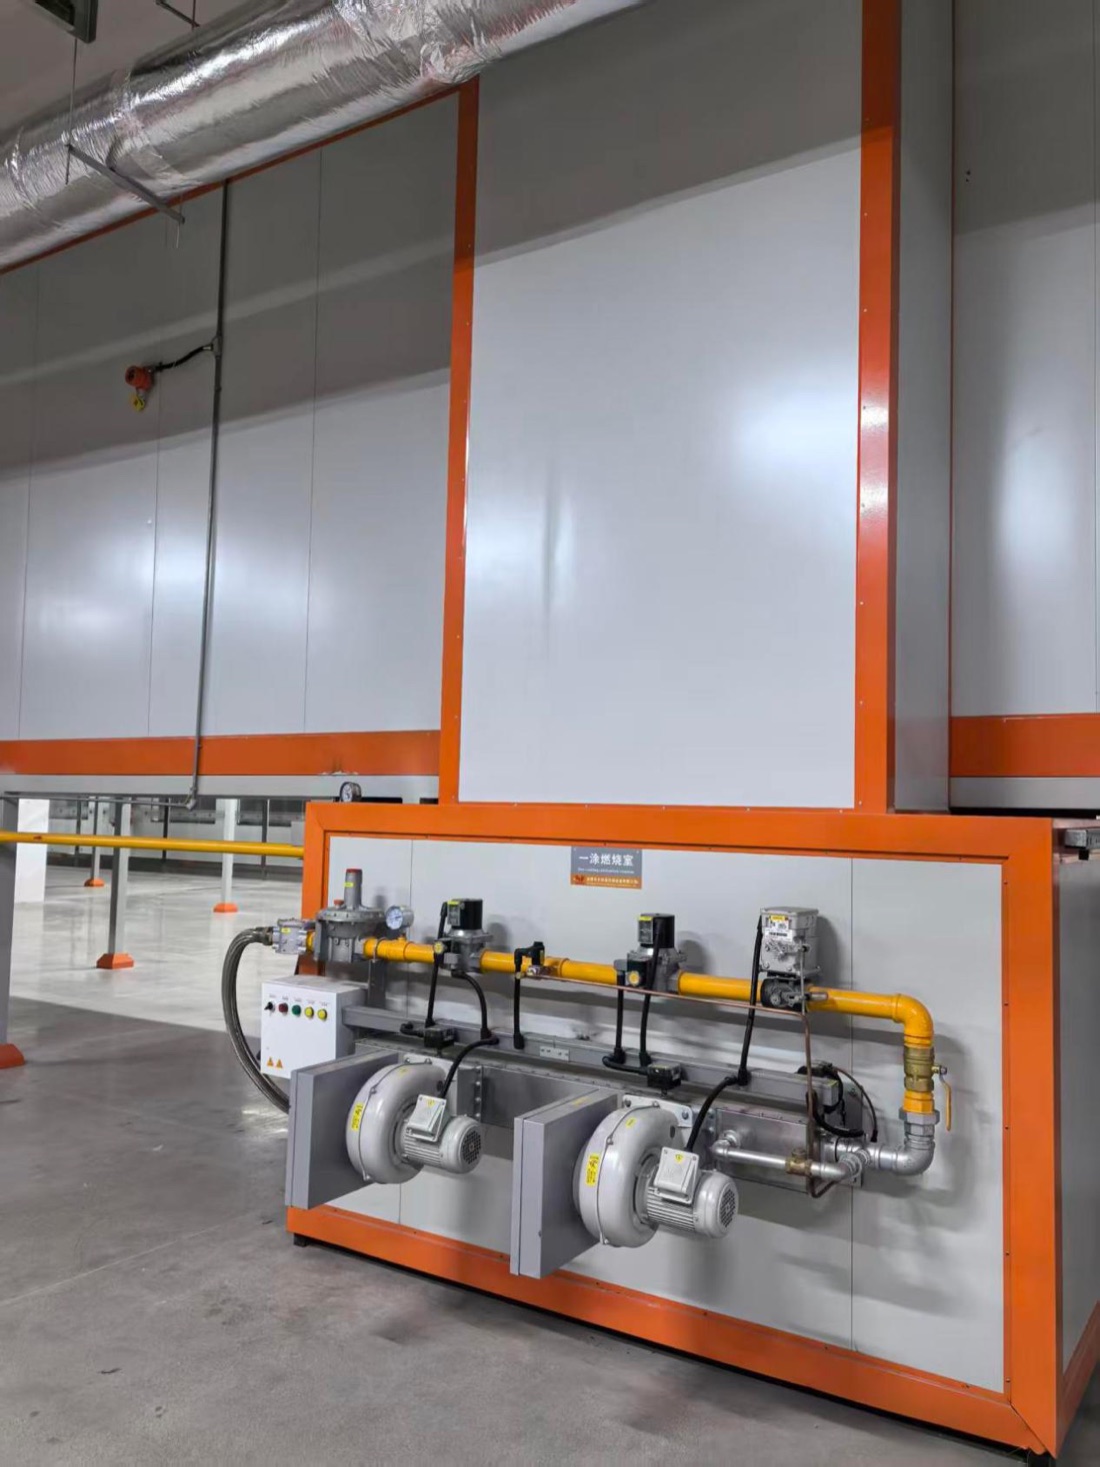
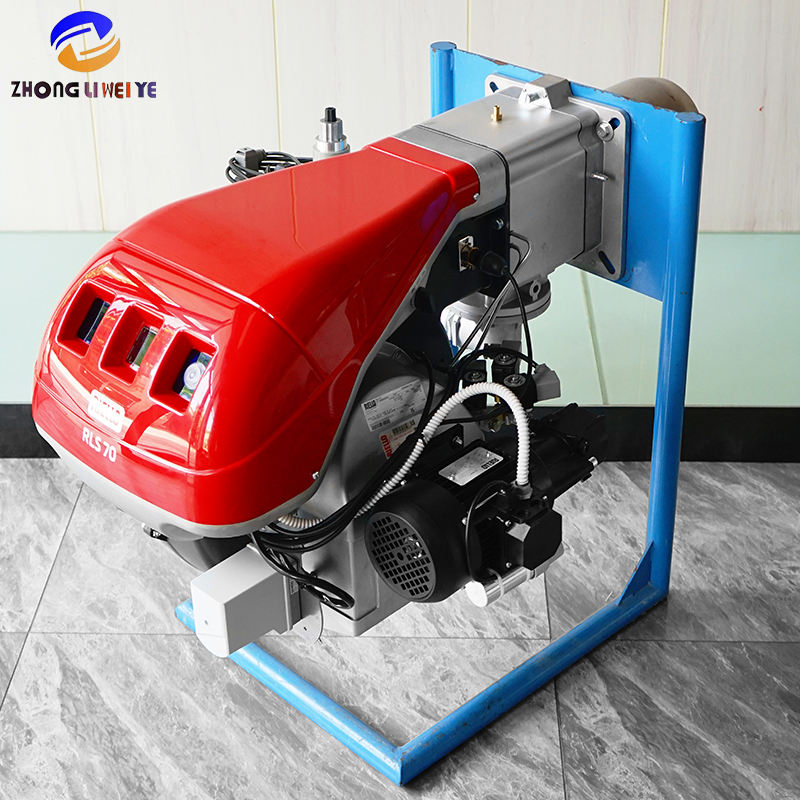
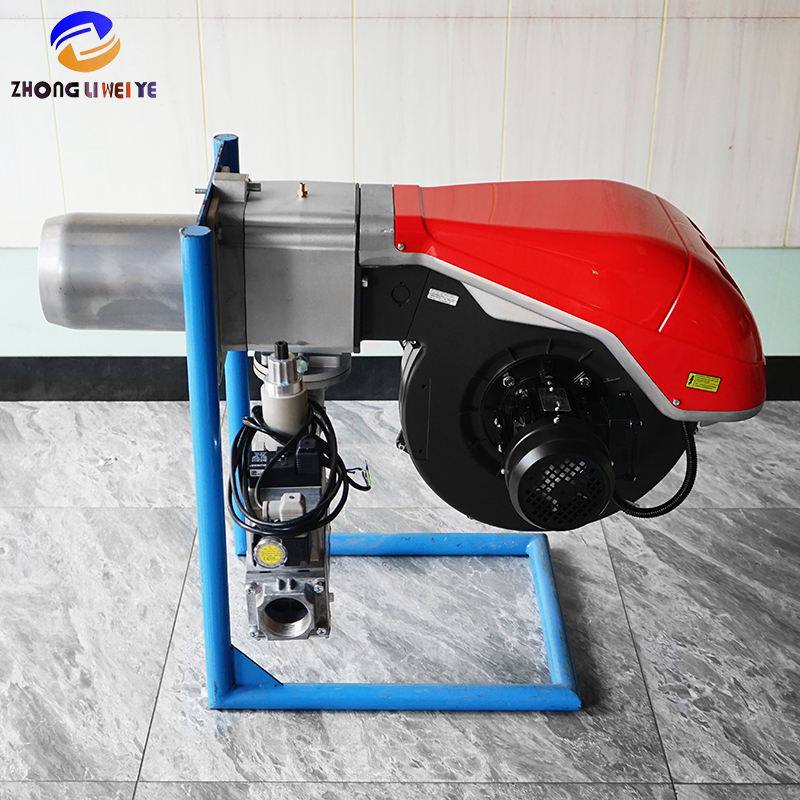
A 2000 m3 asphalt tank needed steady 160C so pumps could move the product in winter. Riello RL100 burners with certified trains held the temperature and cut gas use.
The challenge
In winter the asphalt cooled and pumps could not move it, stalling dispatch.
The old burner's low turndown flameout at hold risked a cold, stuck tank.
Coil-overheat protection was weak on the legacy unit.
Gas use across the tank farm was above budget.
What we supplied & did
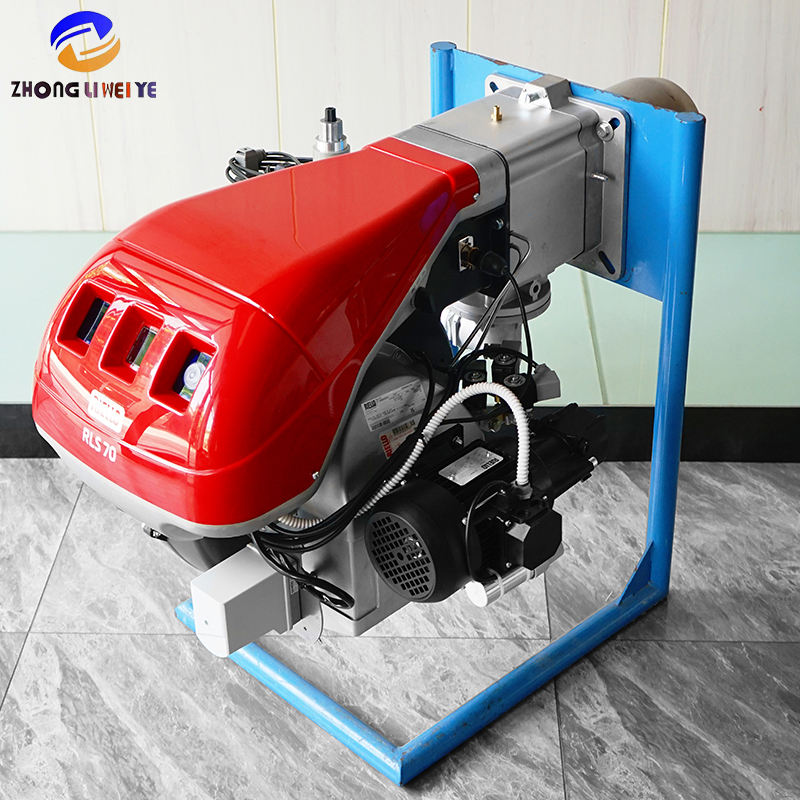
Fitted Riello RL100 modulating burners on the tank heating coils.
Installed Dungs safety valve trains with leak test and dual cutoff.
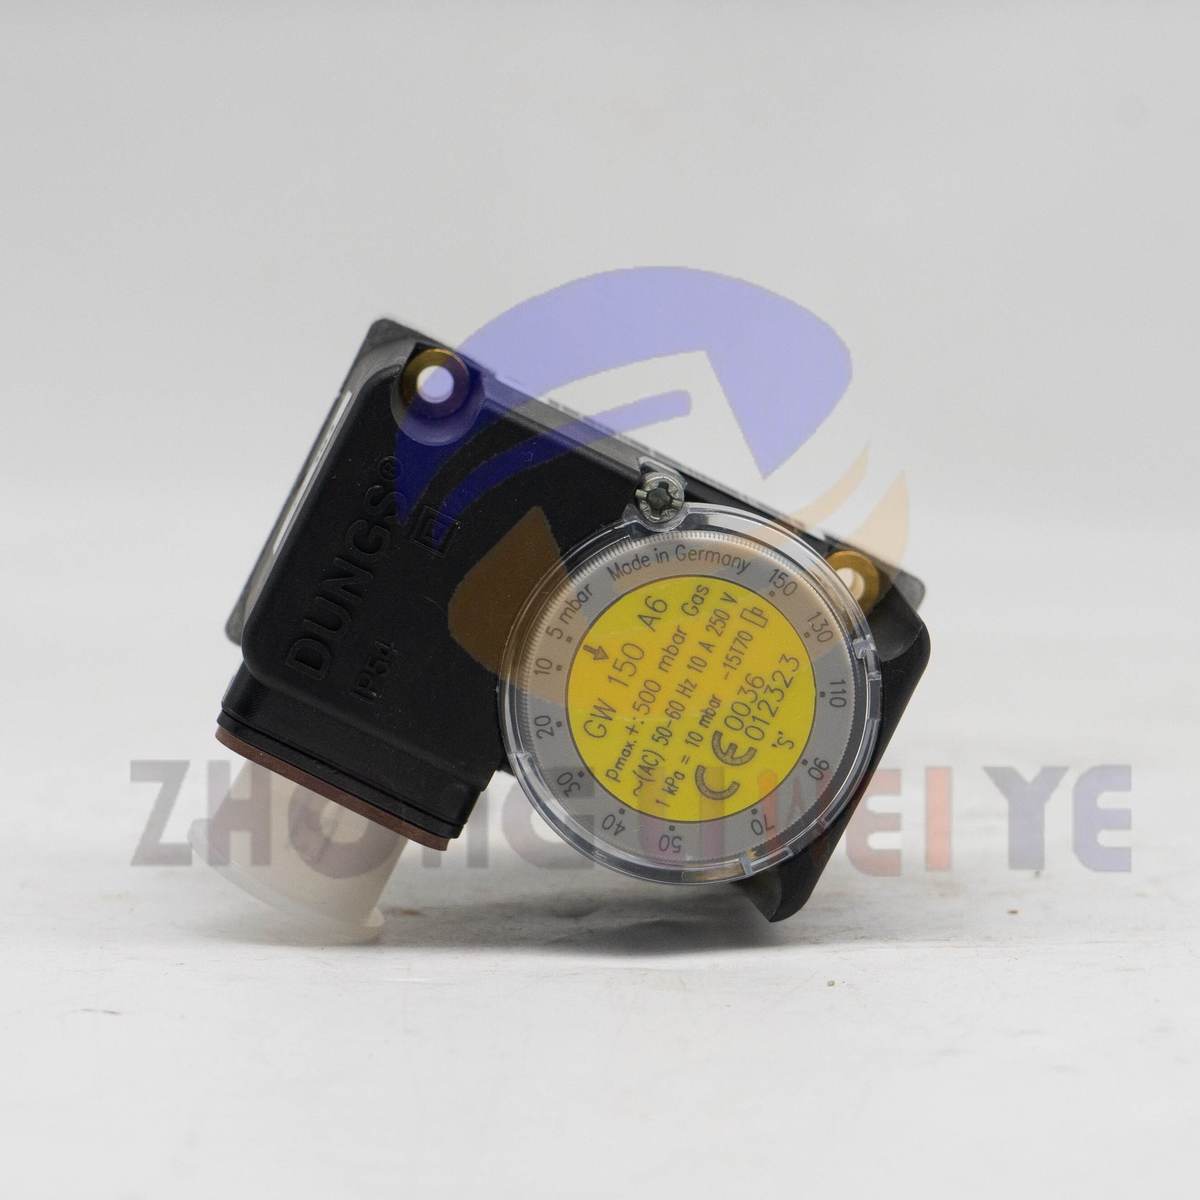
Added Honeywell flame detection and pressure switches with coil-overheat interlock.
Tuned low-load hold to keep the bath at 160C without flameout.
Measured results
What changed on the line
The tank holds 160C through winter, so pumps move product on schedule.
Stable low-load hold removed flameout risk on the cold tank.
Coil-overheat interlock protects the heating coils.
Gas use across the farm fell 8-11%.
Equipment used in this project
Each category page covers what the part does, how it fails and what to check before ordering.
Running a similar duty?
Send the load, the fuel and the process profile — we come back with matching burner, controls and a safety train, and a quotation.
Request a QuoteKeep reading
Related solution
Asphalt Heating
How Zhongli Weiye equips this industry — products, FAQs and a field-proven project.
View solution →