
Case Study · Food Processing
4 t/h Steam Boiler Retrofit for a Food Plant
An aging combustion system was holding back a soy-products and sterilization line. A modulating gas burner with a certified safety train restored stable steam pressure and cut gas use by 8–12%.
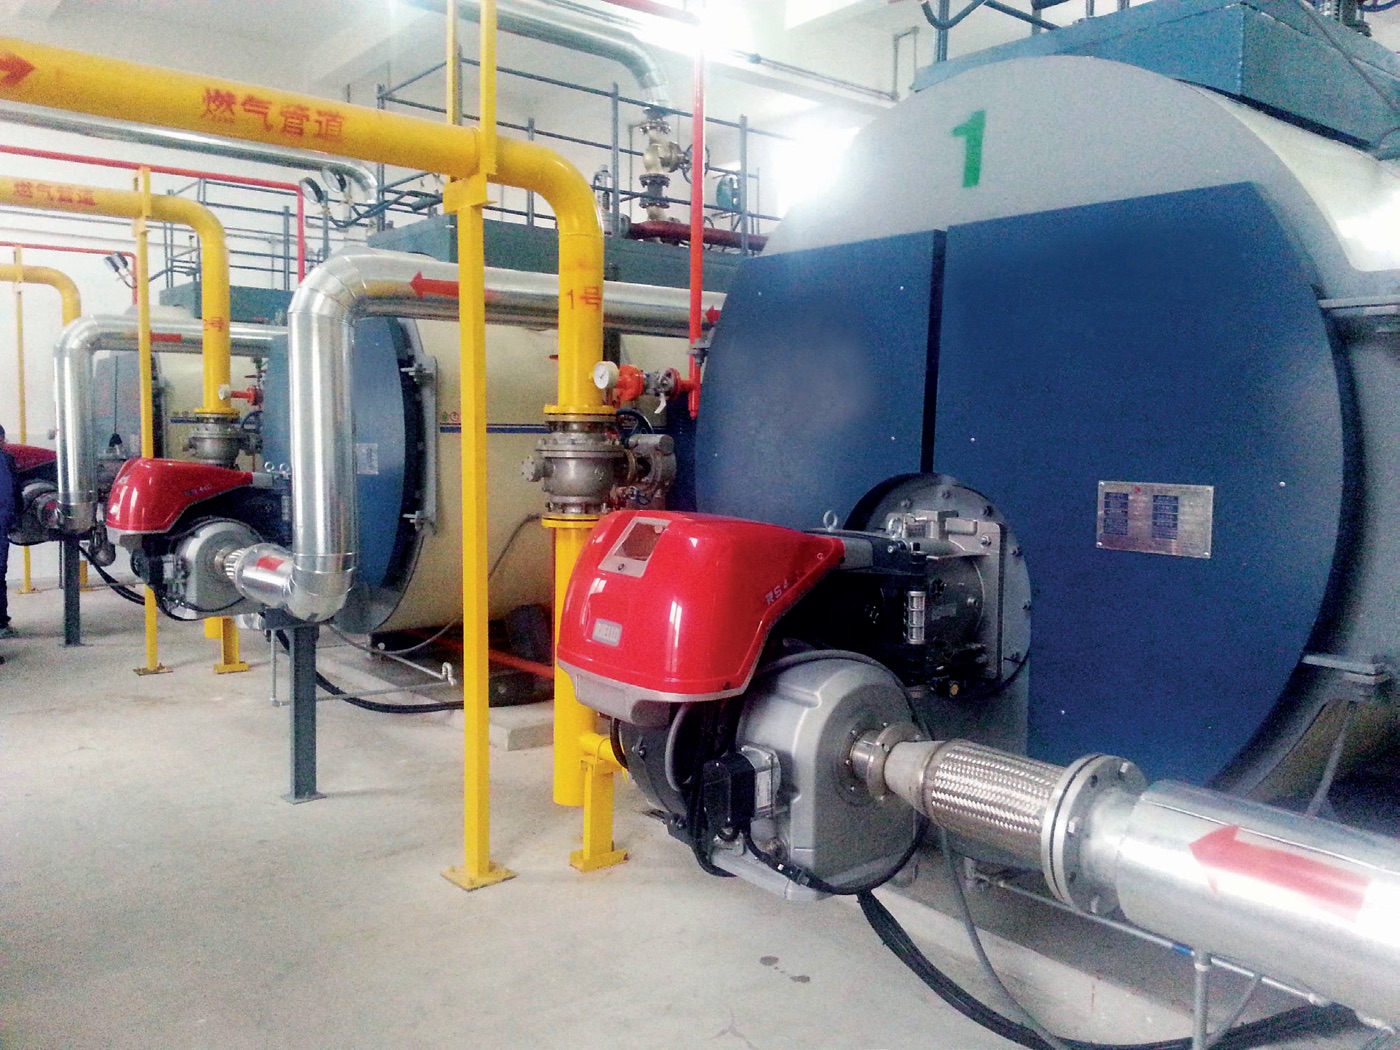
The challenge
Old burner output was unstable; boiler steam pressure swung and the sterilization temperature drifted out of band.
Aged gas valves caused flameouts and ignition faults, driving up maintenance frequency.
Local NOx limits had tightened and the old unit was over the limit, facing rectification.
The line needed stable 4 t/h steam for round-the-clock production.
What we supplied & did
Matched the 4 t/h boiler with a Riello RS120 modulating gas burner for continuous load adjustment.
Fitted a Dungs two-stage safety solenoid valve train for gas cutoff and leak-test protection.
Installed a Siemens combustion program controller covering ignition, flame monitoring and fault interlock.
Tuned the air/fuel ratio on site and applied low-NOx adaptation to meet the local emission limit.
Measured results
What changed on the line
Steam pressure is stable, so the sterilization step no longer depends on pressure swings.
Ignition success is near 100%; flameouts dropped and maintenance load fell.
NOx is within the local limit and passed environmental inspection.
Optimized air/fuel ratio delivered 8–12% gas savings versus the old unit over long runs.
Equipment used in this project
Each category page covers what the part does, how it fails and what to check before ordering.
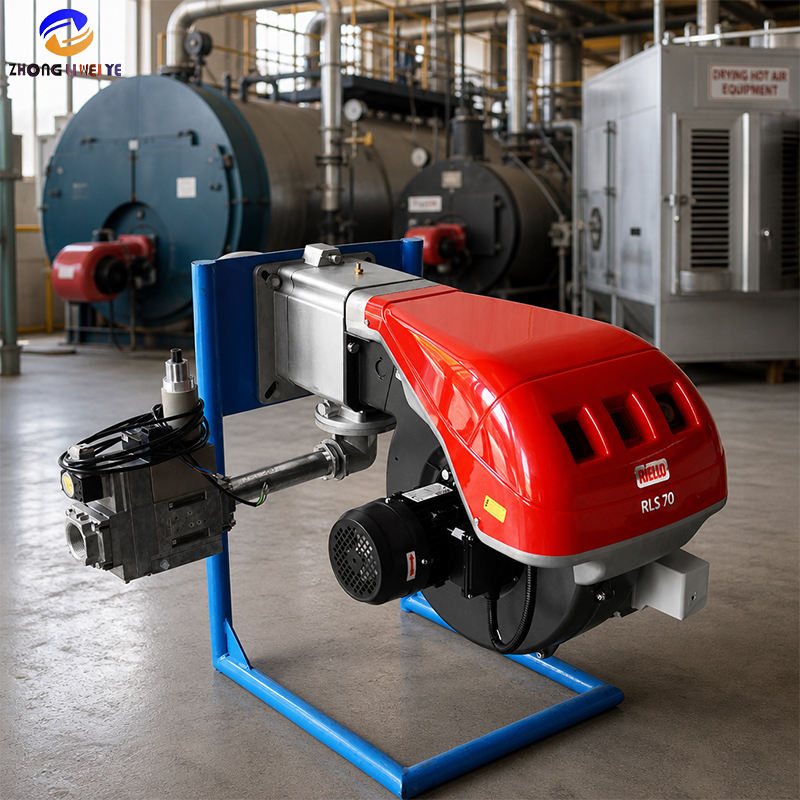
Gas Burners
Modulating firing for stable steam output.
View category →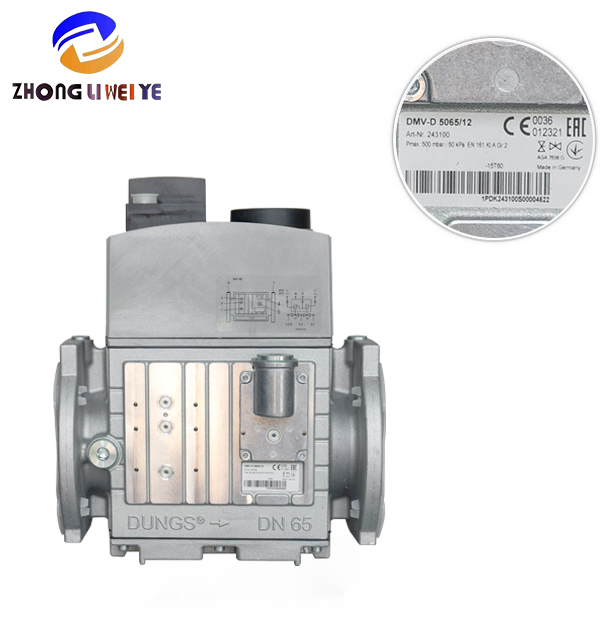
Solenoid Valve
Certified safety shut-off on the gas train.
View category →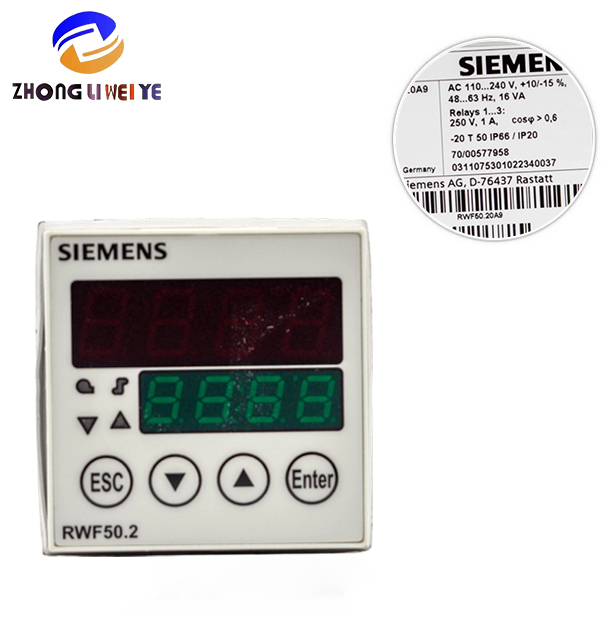
Burner Program Controller
Runs ignition and flame proving every start.
View category →
Flame Detector
Fast flame supervision keeps the safety chain honest.
View category →Running a similar duty?
Send the load, the fuel and the process profile — we come back with matching burner, controls and a safety train, and a quotation.
Request a Quote